A used CNC machine can look like a strong value on the floor and still create an expensive delay after delivery. CNC controller compatibility determines whether the machine can run your existing parts, communicate with your shop systems, accept future service, and return to production on the schedule your operation requires. Before comparing purchase price alone, buyers need to understand what the controller supports and what it will take to make the machine productive.
For a job shop adding capacity, the right controller can shorten setup time and keep operators in familiar territory. For a plant replacing a retired asset, it can determine whether proven programs transfer cleanly or require hours of editing and prove-out. Compatibility is not a single yes-or-no question. It is a practical review of software, hardware, electrical components, communication, operator capability, and long-term service access.
What CNC Controller Compatibility Really Includes
The controller is the command center of a CNC machine. It interprets the part program, manages axis movement, controls spindle and auxiliary functions, monitors alarms, and exchanges data with connected equipment. A control may be widely used and still not be compatible with your specific application.
Start with the installed control family and version. Fanuc, Siemens, Mitsubishi, Heidenhain, Haas, Mazatrol, Okuma OSP, Fagor, and other systems each have different programming conventions, options, interfaces, and service considerations. Even machines using the same controller brand may differ significantly by generation, installed software, axis configuration, or machine-builder parameters.
A machine with a familiar Fanuc control, for example, may still lack the memory capacity, high-speed machining option, probing package, Ethernet capability, or fourth-axis support your work requires. A control that runs standard G-code may not handle every macro, canned cycle, or custom M-code used in your current programs. The productive question is not simply, “Does it have the same brand of control?” It is, “Can this exact machine perform our work without adding unacceptable risk, cost, or delay?”
Program Transfer Is Often the First Test
Part programs are commonly the first compatibility concern because they affect quoting, setup, inspection, and delivery commitments. Standard G-code creates a useful foundation, but it does not guarantee a direct transfer between machines.
Differences can appear in subprogram calls, tool offsets, coordinate systems, macro variables, canned cycles, drilling formats, threading cycles, and alarm behavior. A turning center may use a different approach to tool nose radius compensation than the machine it is replacing. A vertical machining center may require changes to rotary-axis commands, work offset handling, or probing routines. CAM posts must also match the intended control and machine kinematics.
Ask for representative programs rather than assuming that a control label settles the issue. Your programmer, lead operator, or applications team should review the code for control-specific features. If practical, run a sample program during inspection or arrange a dry run before shipment. This is especially worthwhile for complex five-axis work, live-tool turning, mold work, aerospace components, and parts relying on macros or probing.
Program edits are not always a reason to walk away. A straightforward code conversion may be a reasonable trade-off for a well-priced machine with the travel, spindle, tooling, and condition you need. The concern is discovering the scope of that work after the machine is installed and production is waiting.
Confirm Hardware and Motion-System Support
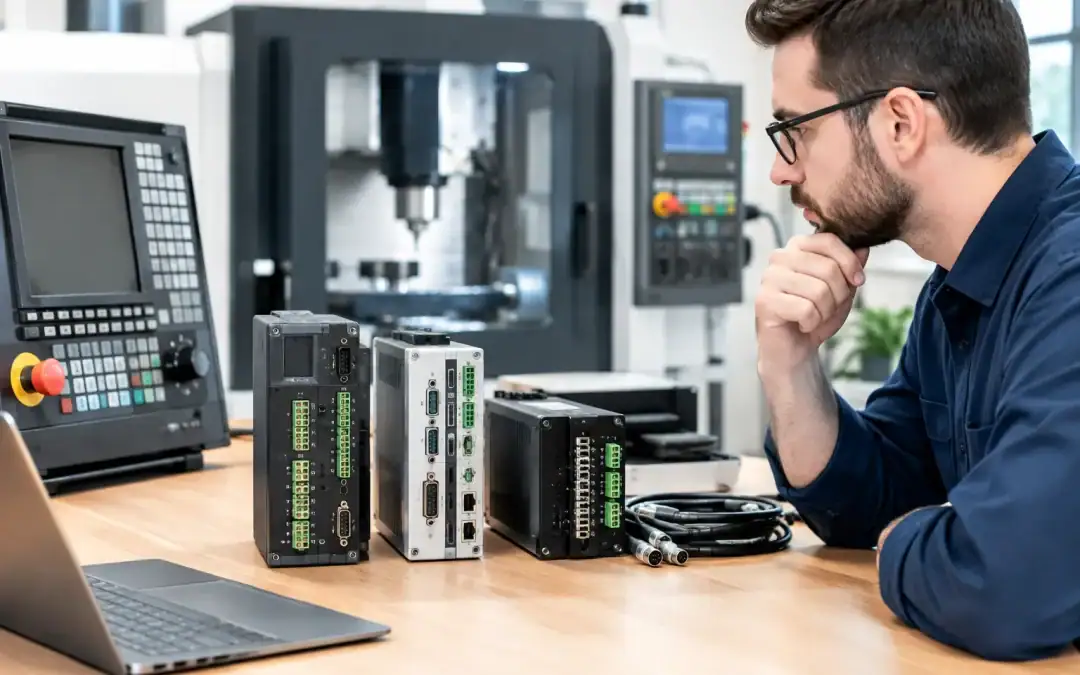
Controller compatibility extends far beyond the screen and keypad. The CNC is connected to servo drives, spindle drives, motors, encoders, I/O boards, power supplies, safety circuits, and machine-builder logic. These components must work together as a system.
When evaluating a used machine, identify the controller model, software version, drive series, motor part numbers, feedback type, and any installed options. Verify whether critical components remain available new, remanufactured, or through reputable surplus channels. Older controls may still be dependable in the right application, but a failed proprietary board or discontinued display can turn a manageable repair into a prolonged outage.
Pay attention to machines that have received partial retrofits. A modern control paired with legacy drives may be a sound solution if the integration was engineered and documented correctly. It can also complicate troubleshooting if wiring diagrams, parameter backups, PLC documentation, and service history are incomplete. Request available electrical prints, manuals, backup files, and records of prior control work.
The machine builder matters here. A controller manufacturer supports the CNC platform, while the machine builder is often responsible for ladder logic, interlocks, hydraulics, lubrication alarms, toolchanger sequences, and custom machine functions. A replacement controller may power up successfully but still require significant engineering before every machine function operates correctly.
Review Connectivity Before It Becomes a Bottleneck
Many shops need more than a controller that can execute a program. They need a machine that fits existing workflow. That may include network program transfer, DNC communication, barcode-driven job setup, probing data collection, tool management, production monitoring, or connection to manufacturing execution systems.
Older controls may rely on RS-232 communication. That is not automatically a problem, particularly for lower-volume work or shops with established DNC systems. But it should be identified before purchase. If your operation expects Ethernet transfer, USB access, remote monitoring, or secure network integration, verify that those capabilities are installed and functional.
Also consider file size and memory. Large CAM-generated programs can exceed the memory on older controls, forcing drip-feed operation or program segmentation. Drip-feeding can work well when properly configured, but it adds another dependency: reliable communication hardware and a process your operators can support.
Security and IT requirements deserve early attention in larger facilities. An older operating environment may not meet internal network policies without an isolated connection or approved gateway. Involving IT and controls personnel before a purchase avoids a situation where a ready machine cannot be connected to the systems your team relies on.
Match the Controller to Your People and Work
A highly capable control is only valuable if your team can use it confidently. Operators trained on one interface may need time to become efficient on another, especially when moving between conversational programming, ISO G-code, and manufacturer-specific workflows.
For a shop with experienced Mazak operators, a Mazatrol-equipped machine may offer faster adoption for the right work. For a facility standardized on Fanuc, keeping a common control family can simplify training, program support, spare-parts planning, and troubleshooting. Standardization is not mandatory, but it has real operating value when uptime and staffing are tight.
The right answer depends on the job mix. A dedicated production cell running stable parts can justify an older, proven control if it is serviceable and the machine is priced appropriately. A high-mix shop with frequent programming changes may benefit more from modern memory, connectivity, probing, and an interface familiar to its operators. A machine purchased for resale or a short-term contract may call for a different calculation than a long-term capital asset.
Questions to Ask Before Buying a Used CNC Machine
A disciplined pre-purchase review protects both budget and schedule. Before committing, confirm these points with the seller and your internal team:
- What is the exact controller model, generation, software version, and installed option list?
- Can the machine run representative programs or parts from your current workload?
- Which communication methods are installed and tested: Ethernet, USB, RS-232, DNC, or wireless adapters?
- Are controller backups, parameters, ladder files, manuals, electrical prints, and service records available?
- What drives, motors, encoders, and boards are installed, and how accessible are replacement parts?
- Does the control support the required axes, probing, toolchanger functions, live tooling, pallet systems, or automation interface?
- Will your existing CAM post processor work, or does it need revision?
- Who will install, power up, level, commission, and support the machine if a control issue appears?
These questions also help sellers present equipment accurately. Clear controller details, photographs of the control screen, option information, available documentation, and operational videos reduce uncertainty for serious buyers. Transparent information supports a faster transaction and a more realistic price.
When a Control Retrofit Makes Sense
A retrofit can extend the useful life of a mechanically sound machine, add modern connectivity, and reduce dependence on aging electronics. It is most attractive when the base machine has valuable iron: good geometry, adequate travels, a capable spindle, quality mechanical condition, and a configuration suited to the work.
However, a retrofit is an engineering project, not a simple control swap. Costs can include the control, drives, motors, wiring, electrical cabinet work, safety updates, programming, commissioning, operator training, and downtime. Toolchanger logic, rotary tables, automatic pallet changers, and custom automation can add complexity quickly. In some cases, purchasing a machine with a supported native controller is the faster and more capital-efficient choice.
Revelation Machinery helps buyers evaluate used CNC equipment with the practical details that matter before it reaches your floor. A clear discussion of control type, available records, machine condition, application needs, and delivery requirements can prevent a purchase that looks economical but slows production.
The best used CNC purchase is not necessarily the newest control or the lowest price. It is the machine whose controller, mechanics, documentation, and support path fit the way your operation actually makes parts. Verify that fit before the truck arrives, and the equipment has a far better chance of becoming capacity instead of a project.