A spindle can look clean, run quietly at idle, and still become the most expensive issue on a used CNC machine. Before committing capital, buyers need to assess machine spindle wear with the same discipline they apply to control age, travel, tooling, and machine geometry. A careful evaluation protects production schedules, strengthens price negotiations, and helps determine whether a machine is ready for work, needs planned service, or should be passed over.
For a vertical machining center, horizontal, turning center, or multi-axis lathe, spindle condition affects more than surface finish. It can influence cycle times, tool life, part accuracy, vibration, and the ability to hold tolerances over a full production run. The goal is not to expect a used spindle to perform like a new one. The goal is to understand its present condition, its likely service horizon, and the financial exposure attached to it.
Why spindle condition changes the real cost of a used machine
A machine with a healthy spindle can be an excellent value, even with substantial hours on the meter. Conversely, a lower-priced machine with an unknown or deteriorating spindle may require a repair that changes the economics quickly. Spindle rebuilds, replacements, removal and installation labor, balancing, testing, and lost production time all need to be considered.
The cost and complexity depend on the machine. A belt-driven spindle may be relatively straightforward to service, while an integrated motor spindle, high-speed HSK spindle, or specialty turning spindle can involve more lead time and expense. OEM support, parts availability, taper style, maximum RPM, and the machine’s application all matter.
This is why spindle assessment should not rely on a single observation. A seller’s statement that the machine is “under power” is useful, but it is not a condition report. Ask for evidence, observe the machine through a meaningful test cycle when possible, and match the inspection depth to the value and intended use of the equipment.
How to assess machine spindle wear during inspection
The strongest assessment combines operating history, physical inspection, test cuts, and measured data. No one check tells the full story. A machine used for aluminum at high RPM can show different wear patterns than one used for interrupted cuts in steel or cast iron.
Start with machine history and application
Ask how the machine was used, what materials it cut, and whether it ran one shift or around the clock. High hour counts alone do not condemn a spindle, but they provide context. A well-maintained machine running consistent work may be a better prospect than a lower-hour machine with unknown maintenance practices or a history of crashes.
Request maintenance records when available. Look for documentation of spindle rebuilds, bearing replacements, drawbar service, lubrication repairs, vibration issues, alarms, or prior crash damage. A documented rebuild by a qualified provider can be a positive factor if the work, date, and scope are clear.
Also ask about the tooling and processes used. Heavy roughing, large face mills, aggressive drilling, frequent tool changes, and sustained high-speed operation put different demands on the spindle. In a turning center, bar work, interrupted cuts, and chucking practices can be just as relevant.
Inspect the taper, nose, and tool interface
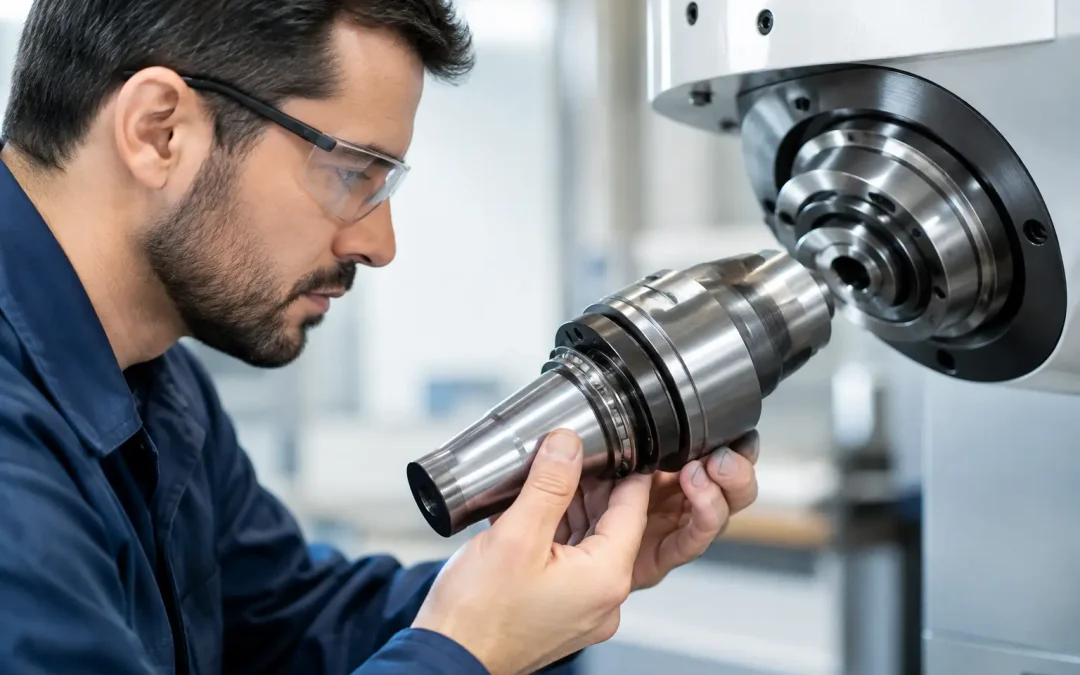
With the machine safely powered down and a tool removed, inspect the spindle taper or tool interface closely. The taper should be clean, smooth, and free of fretting, corrosion, scoring, or obvious impact marks. Damage in this area can reduce toolholder contact, contribute to runout, and accelerate wear.
For CAT, BT, or similar tapers, examine the witness pattern on a clean toolholder after a controlled insertion. Uneven contact marks may indicate taper damage or contamination, though they should be evaluated by an experienced technician before drawing conclusions. For HSK systems, inspect the contact surfaces, clamping features, and toolholder condition with equal care.
On lathes, inspect the spindle nose, chuck mounting surfaces, and any signs of damage around the drawtube or collet system. A worn chuck can create runout that is mistaken for a spindle problem, so separate the condition of the workholding from the condition of the spindle itself.
Listen through the speed range
Run the spindle through low, middle, and high RPM ranges, allowing it to stabilize at each point. Listen for growling, rumbling, whistling, knocking, or a change in sound as speed increases. Bearing noise may be subtle at low speed and become more noticeable as RPM rises.
Do not judge sound in isolation. Shop noise, coolant pumps, hydraulics, gearbox components, and enclosure resonance can complicate the test. Still, an experienced operator can often identify a sound that is inconsistent with normal operation. Video recorded near the spindle during a speed sweep can also be helpful when an in-person inspection is not possible.
Pay attention to acceleration and deceleration. Unusual vibration, alarms, excessive coast-down behavior, or repeated difficulty reaching commanded speed deserve follow-up. A machine should also hold commanded RPM consistently rather than hunting or fluctuating.
Check spindle temperature and vibration
After operating at a representative speed and load, check for excessive heat around the spindle housing. Some warmth is normal, particularly on high-speed machines. The concern is abnormal temperature rise, a clear hot spot, or a machine that reaches an alarm condition after a relatively short run.
A vibration analyzer provides more useful evidence than touch or sound alone. It can identify bearing-related frequencies, imbalance, looseness, and other conditions that may not be visible. For higher-value equipment or machines intended for close-tolerance work, arranging vibration analysis is a sensible investment.
Thermal imaging can provide another useful reference point. Compare temperatures across the housing and, if possible, against similar equipment operating under comparable conditions. Results must be interpreted carefully because ambient temperature, spindle speed, lubrication design, and machine construction affect the reading.
Measure runout correctly
Runout testing is one of the most valuable parts of a spindle inspection, but the setup matters. A dial indicator against the taper, a precision test bar, or a toolholder-held gauge can each provide information. Use clean, undamaged inspection tooling and confirm that the measuring method matches the machine type.
Measure at more than one location. Taper runout, test-bar runout near the nose, and runout farther from the spindle can point to different causes. A result that worsens dramatically farther from the spindle may involve the toolholder, test bar, setup, or bending rather than the spindle bearings alone.
There is no single acceptable runout number for every machine. Required tolerance depends on the spindle design, taper, age, intended process, and the work your shop plans to run. A machine producing general fabrication parts may be suitable with condition levels that would not work for aerospace, medical, mold, or precision toolroom applications.
Request a real test cut
If practical, a test cut is more revealing than a no-load demonstration. Use a known tool, appropriate material, and a program that reflects the work the machine will perform. Observe surface finish, chatter, dimensional consistency, and spindle load. For mills, bore interpolation or circular pocketing can expose issues that a simple facing operation may not reveal.
For lathes, turn a test diameter and check taper, finish, and repeatability. If possible, make multiple passes and re-measure after the machine has warmed up. This helps distinguish a one-time setup issue from a condition that changes under heat or cutting load.
Separate spindle symptoms from other machine problems
Not every finish issue or runout reading originates in the spindle. Poor toolholders, worn pull studs, damaged retention knobs, weak drawbar force, loose machine leveling, ball screw backlash, turret alignment, fixture rigidity, and programming can produce similar symptoms.
Drawbar retention force deserves particular attention on machining centers. Insufficient clamping force can allow micro-movement between the toolholder and taper, contributing to chatter, taper wear, and poor finish. A drawbar force gauge provides a direct measurement and may reveal a service need that is less severe than a spindle replacement.
Likewise, inspect the machine’s lubrication system and verify that alarms are absent. Bearing damage can result from lubrication failures, contamination, coolant intrusion, or crash events. Finding the underlying cause matters because replacing a spindle without correcting the cause invites another costly failure.
Match inspection depth to purchase risk
For a lower-cost machine intended for straightforward work, a thorough operational demonstration, taper inspection, sound check, and test cut may provide sufficient confidence. For a high-dollar five-axis machine, high-speed VMC, or equipment required to hold tight tolerances from day one, a more formal inspection is justified.
Consider bringing an independent service technician or a trusted maintenance lead to inspect the machine. The cost is small compared with unexpected downtime after delivery. If an on-site inspection is not available, request current videos of cold start-up, spindle speed sweeps, tool changes, and test cuts, along with photos of the taper and maintenance documentation.
When a concern appears, it does not automatically make the machine a poor purchase. It may create a negotiating point, support a planned maintenance budget, or help you decide whether the seller should complete repairs before shipment. The key is transparency about what is known, what remains uncertain, and what the machine will need to support your production requirements.
A dependable used equipment partner should help make those decisions faster, not harder. Revelation Machinery works to provide the responsive communication and practical equipment guidance manufacturers need when uptime and capital efficiency are on the line. Before placing a machine on your floor, make spindle condition part of the purchase decision – then move forward with a clear plan for production, service, and long-term value.