A press brake that looks right on paper can still become a production bottleneck on the floor. A machine may have enough nominal tonnage but lack the bed length, throat depth, tooling compatibility, or control capability your parts require. Knowing how to choose press brake equipment starts with the work you need to bend repeatedly, not the machine listing that happens to be available today.
For most shops, the best purchase balances current part requirements, expected growth, available labor, and the real cost of getting the machine operational. That is especially true when evaluating used equipment, where a well-maintained, properly sized machine can deliver more value than an oversized purchase with unnecessary features.
Start With the Parts You Bend Most Often
Review production history before comparing press brake brands, models, or prices. Identify the material types, thickness ranges, longest bend lengths, flange dimensions, and bend quantities that drive your work. A press brake should be selected around the parts that generate the most revenue or create the most scheduling pressure.
Material matters as much as thickness. Mild steel, stainless steel, aluminum, galvanized sheet, and high-strength materials require different forming force. Stainless and high-tensile materials, for example, can require substantially more tonnage than comparable mild steel. Do not size a brake using a single tonnage chart without confirming the material’s tensile strength, grain direction, bend radius, and tooling setup.
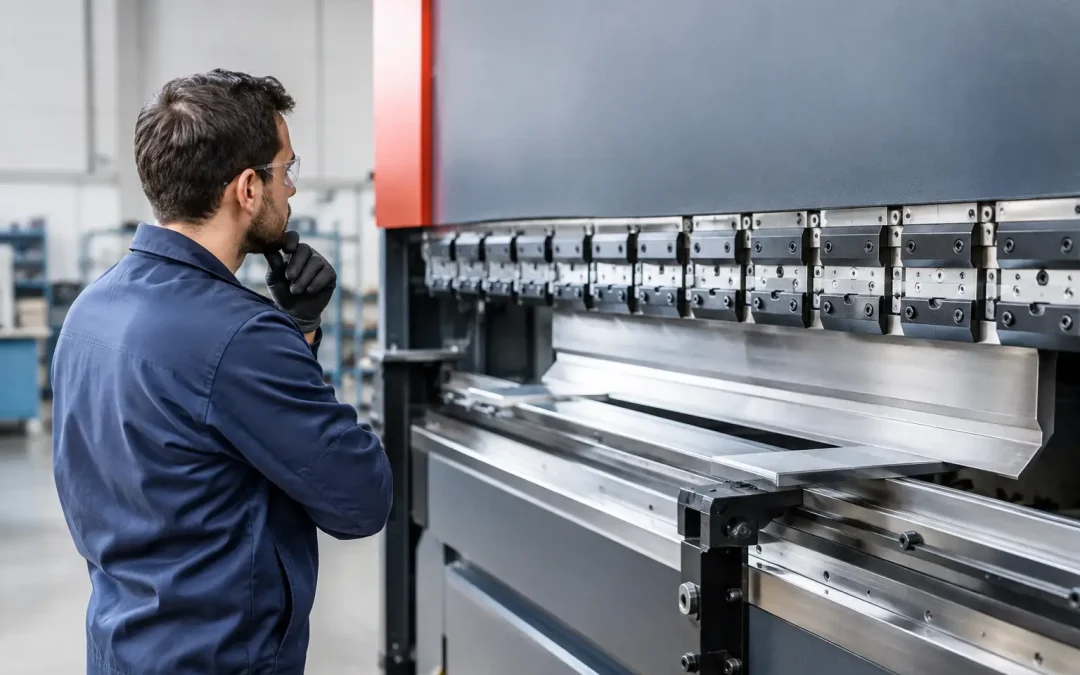
Look closely at the longest part, but do not stop there. A 10-foot bed does not automatically mean the machine will comfortably form every 10-foot part. Side frames, tooling clearance, part geometry, and the need to position work around the machine all affect usable capacity. If your work includes large panels, deep boxes, or return flanges, open height, stroke, daylight, throat depth, and distance between frames deserve as much attention as bed length.
How to Choose Press Brake Tonnage and Length
Tonnage is the first specification most buyers ask about, and it is essential. It is also commonly misunderstood. Press brake tonnage is the total force available across the bend, not a blanket rating for every material and bend condition. The required force changes with material thickness, bend length, die opening, and the forming method.
Air bending is the most common method in modern fabrication because it provides flexibility with lower tonnage than bottoming or coining. As a general starting point, a V-die opening near eight times the material thickness is often used for mild steel air bending, but that rule is not a substitute for manufacturer tonnage tables and experienced setup practices. The wrong die opening can affect bend radius, required force, and finished part quality.
Avoid buying only for the average job. A machine operating at or near maximum tonnage every day leaves little room for material variation, difficult jobs, or growth. On the other hand, buying far more capacity than necessary can tie up capital, increase operating costs, and limit your used-equipment options. The practical target is a press brake that handles routine work efficiently and accommodates the demanding jobs that make a meaningful difference to your schedule.
Bed length should follow the same logic. Consider whether you need full-length bending, staged bending with multiple tool setups, or the ability to run two smaller jobs simultaneously. A longer bed offers flexibility, but it may require more floor space, handling capacity, and tooling investment. For a shop focused on short brackets and small enclosures, a shorter high-quality brake may be the better operational decision.
Match the Machine to Your Production Method
The right press brake depends on how parts move through your shop. A low-volume job shop with frequent changeovers has different needs than a production facility running repeat orders all day.
For frequent setup changes, prioritize a capable CNC control, easy tooling changes, and reliable backgauge movement. A multi-axis backgauge can reduce setup time and help operators produce more complex parts consistently. Programmable bend sequences, graphical interfaces, and offline programming can also be valuable when parts vary often or when experienced operators are in short supply.
For repetitive production, speed, repeatability, and material handling may matter more than advanced programming features. Consider ram approach speed, bending speed, return speed, crowning capability, and the machine’s ability to maintain consistent angles across long bends. Hydraulic press brakes remain widely used and capable, while electric and hybrid models may offer faster cycle times, energy savings, and lower maintenance demands for the right application. The best choice depends on your duty cycle, material mix, and available service support.
Also account for operator workflow. A machine that requires awkward handling can slow production even when its specifications appear ideal. Large or heavy parts may require front supports, sheet followers, lifting assistance, or a team-based workflow. If one operator cannot safely manage the workpiece, the purchase decision should include the cost of supporting equipment and labor.
Tooling Compatibility Is a Production Decision
Tooling is not an accessory after the press brake purchase. It is part of the production system. Before committing to a machine, confirm the punch and die style, clamping system, tool height, and availability of the tooling needed for your parts.
A press brake with common, readily available tooling standards can simplify future expansion and replacement. If you already own a substantial tooling inventory, compatibility may narrow the best machine choices immediately. If you are building a new setup, plan for the punches, dies, holders, gooseneck tools, radius tools, and specialty tooling your work requires.
Pay attention to segmented tooling and quick-clamp systems if your work involves short bends, complex profiles, or frequent changes. These features can reduce setup time, but they only create value when they fit the work your shop actually performs. A simpler tooling arrangement may be more economical for long production runs with limited part variation.
Evaluate Used Press Brake Condition Beyond the Nameplate
Recognized brands often retain value because parts, technical knowledge, and resale demand are easier to find. However, brand reputation should not replace a careful inspection. A used press brake should be evaluated as an operating asset, not simply a discounted version of a new machine.
When possible, inspect the machine under power and ask to see it cycle, gauge, and form a representative part. Review available maintenance records, control documentation, electrical diagrams, tooling included in the sale, and any known repair history. A professional assessment can prevent costly surprises after delivery.
Focus on these areas during a used-machine evaluation:
- Ram and bed condition, including signs of damage, uneven wear, or alignment concerns.
- Hydraulic system performance, leaks, hose condition, pump noise, and operating pressure.
- Backgauge accuracy, repeatability, finger condition, and axis movement.
- Control operation, error history, software condition, and availability of replacement components.
- Safety equipment, including guards, light curtains, foot pedals, emergency stops, and compliance needs.
A machine may need minor service, new tooling, or updated safety components. Those costs are not necessarily deal breakers. The key is to identify them before the purchase and compare the full installed cost against alternatives.
Plan for Installation, Power, and Service
A press brake purchase is not complete when the machine leaves the seller’s facility. Confirm the machine’s weight, dimensions, rigging requirements, electrical voltage, phase, amperage, and compressed-air needs. Verify that your floor can support the load and that access doors, ceiling clearances, and travel paths can accommodate delivery.
Service access is equally important. Ask who will support controls, hydraulics, electrical issues, and replacement parts after installation. Older machines can be excellent values when documentation and parts support remain available. A lower-priced machine with an obsolete control or limited service options can create more downtime risk than its upfront savings justify.
If you are buying used equipment for an urgent capacity need, work with a machinery partner that can provide clear machine information, responsive communication, and coordination from quote through delivery. Revelation Machinery helps manufacturers source dependable used fabrication equipment with the speed and transparency needed to keep production moving.
The right press brake should make your next production schedule easier, not force your team to work around its limitations. Bring real part drawings, material details, and workflow requirements into the buying conversation. That preparation gives you a stronger basis for comparing machines and a better chance of putting productive capacity on the floor quickly.